News Center
Recommending Products
Contact: Mr. Jin
Tel: 13901575780
0512-52428686
Contact: Mr. Zha
Tel: 13913639797
0512-52422071
Address: No. 59, Huyi Road, Liantang, Shanghu Town, Changshu City, Jiangsu Province.
How to control the parallelism between the blades of a double angle circular knife when multiple bla
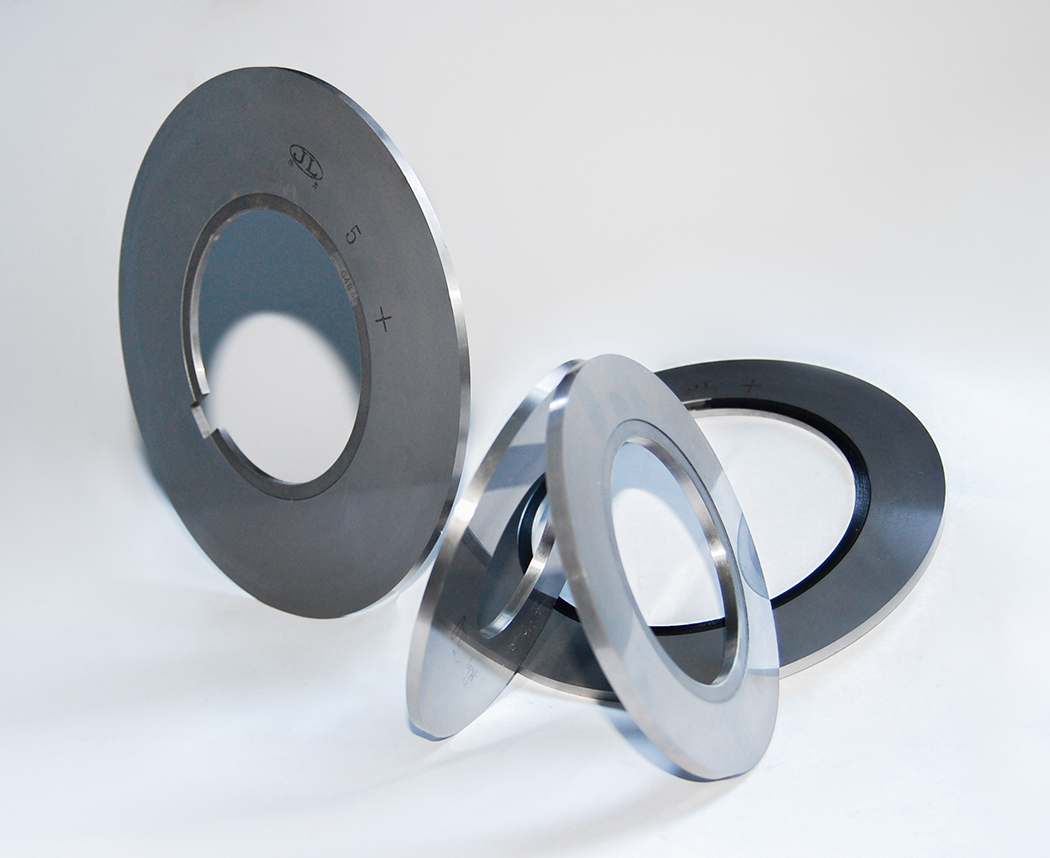
Double angle circular knives are commonly used in multi column cutting scenarios for lithium electrode sheets, thin films, and adhesive tapes. Dozens of blades are installed side by side on the blade axis, and the parallelism of the blades directly determines the uniformity of the bite gap and the consistency of the burr on the incision. In severe cases, local crushing, blade breakage, and continuous cutting may occur. Control is divided into full chain control of part benchmark, tool axis benchmark, spacer accuracy, assembly process, testing, and operation compensation.Sources:www.cssjlgj.com | PublishDate:2026.11.09
1. Upstream component benchmark control (source)
1. Flatness and end face runout of the blade itself
The two end faces of the double angle circular knife are the assembly reference surfaces, and the parallelism and flatness of the end faces must be ensured to meet the standards before leaving the factory; The focus of the thin hard alloy double angle circular cutter is to control grinding warpage, and to perform stress relief treatment after grinding to avoid deformation after assembly under stress. If the blade itself has a curved end face, no matter how it is assembled, parallelism cannot be guaranteed.
2. The precision of the spacer (gasket) is the core of dense tool matching
A large number of positioning sleeves are used for dense knife matching, and high requirements are placed on the parallelism, end surface roughness, and wall thickness uniformity of both ends of the sleeve; The end faces of the spacer are not parallel, and with each stack, errors accumulate, and the errors of the multi blade group are amplified step by step.
Choose a whole precision grinding spacer and do not use multi-layer thin pads stacked with cutting tools (multi-layer pad stacking can easily cause misalignment and cumulative parallelism errors);
The material of the spacer is stable, avoiding deformation under pressure; The clearance between the inner hole of the spacer and the blade shaft is reasonable, and excessive clearance can easily cause deviation.
3. Knife shaft body benchmark
The cylindricity of the blade shaft, the perpendicularity of each shoulder end face to the axis, and the radial runout of the blade shaft must be verified in advance; The blade axis is bent and the shoulder end face is tilted, causing all blades to tilt as a whole after assembly, resulting in synchronous failure of multi blade parallelism.
2. Assembly process control (key focus of intensive tool matching)
1. Assembly sequence and cleaning
Before assembly, wipe the blade end face, both ends of the spacer sleeve, and the shoulder of the blade shaft clean and free of dust, metal debris, and burrs; Small impurities trapped on the bonding surface can cause single point elevation and blade tilt.
2. Locking method and torque control
When locking multiple blade groups, it is not possible to lock them all at once. Instead, a step-by-step uniform pre tightening and step-by-step pressure application should be used, with alternating locking from the middle to both ends or both ends, to avoid the blades being pushed off center or warped by force; The locking torque strictly follows the process. If the torque is too large, the thin blade will undergo elastic deformation and end face warping; Insufficient torque, blade displacement and parallelism deviation after running vibration.
3. Positioning method
Dense blade matching generally uses keyway or flat key circumferential positioning to prevent blade rotation; The gap between the key and keyway should not be too large to avoid lateral displacement of the blade and damage to parallelism.
Taboo: Dense multi blade groups are not suitable for aligning by hand pushing. Forcefully bending the blades to correct parallelism by external force can generate internal stresses during assembly and result in inaccurate rebound after high-speed operation.
3. Testing methods
1. Static inspection (after assembly, do not use the machine)
Use a dial gauge/micrometer, fix the gauge holder, and run the end face of each blade radially and axially along the blade; Using the reference blade (first blade) as a reference, compare the axial deviation of the other blade end faces to indirectly reflect the parallelism between the blades.
2. Dynamic detection of the entire machine under no-load conditions
Low speed rotary blade shaft, retest end face runout in rotating state, distinguish static assembly errors and deformation caused by force and rotation; Eliminate the interference caused by the jumping of the blade shaft itself.
3. Auxiliary verification
Matching bottom blade/bottom roller, check the bite gap between each double angle circular blade and the bottom roller. If there is a significant difference in the gap between multiple blades, it is a visual manifestation of the blade parallelism exceeding the tolerance.
4. Control of operating conditions and processes
1. Control temperature rise
Friction heating during high-speed slitting can cause inconsistent thermal expansion of the blade shaft, spacer, and blade, which can alter the state of the joint surface and cause parallelism drift; Long term high-speed slitting can increase blade shaft cooling.
2. Prevent vibration
The rigidity of the frame and knife holder is insufficient, and the vibration during operation will cause the locking surface to loosen, gradually deteriorating the parallelism; The dense multi blade group has higher requirements for the rigidity of the blade holder.
3. Regular re inspection
Dense blade matching belongs to a high cumulative error structure, and parallelism must be rechecked after material replacement, regrinding of blades, and disassembly; Perform daily inspections and synchronously compare the quality of each cutting edge (burrs, indentations) as a warning for abnormal parallelism.
5. Error allocation logic
Multi blade dense matching belongs to the error accumulation system:
The total deviation is formed by the combination of single blade end face error, spacer end face error, tool axis perpendicularity error, and locking deformation error.
Error allocation should be done during design to reduce the number of series stacking; The more knife groups there are, the stricter the requirements for the end face accuracy of individual parts.