News Center
Recommending Products
Contact: Mr. Jin
Tel: 13901575780
0512-52428686
Contact: Mr. Zha
Tel: 13913639797
0512-52422071
Address: No. 59, Huyi Road, Liantang, Shanghu Town, Changshu City, Jiangsu Province.
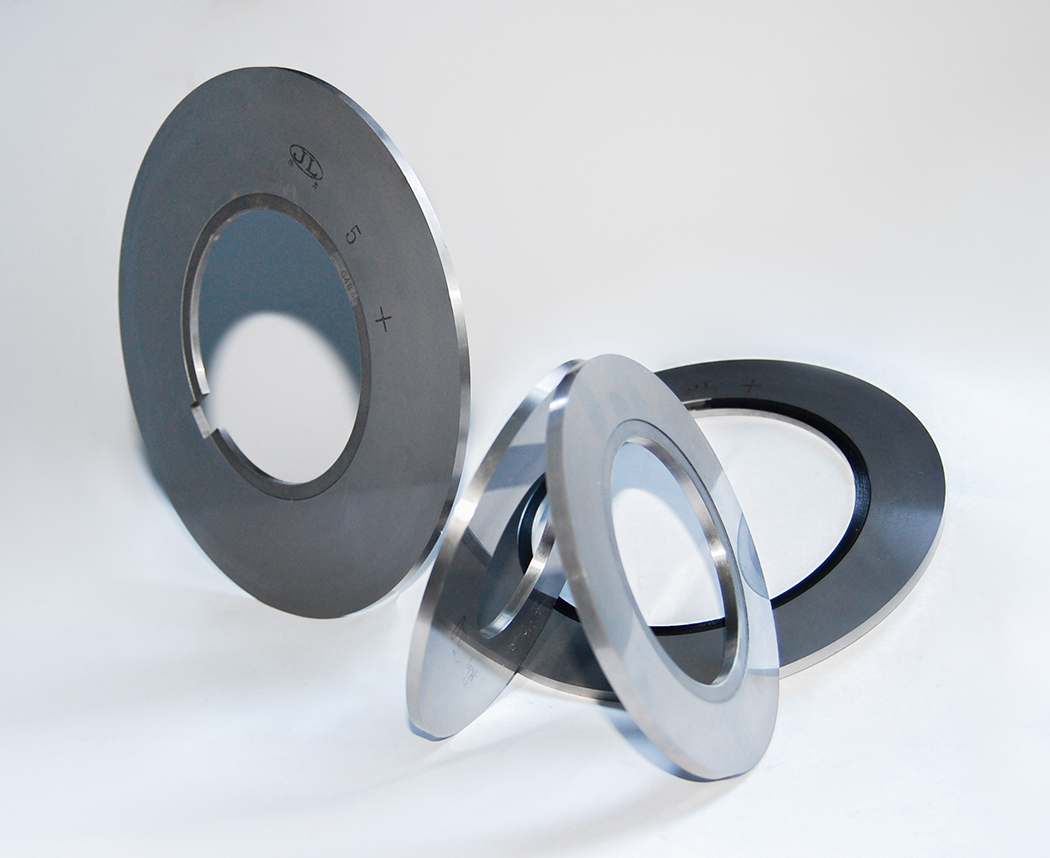
Which workpiece materials are suitable for high-speed steel saw blade milling cutters to process
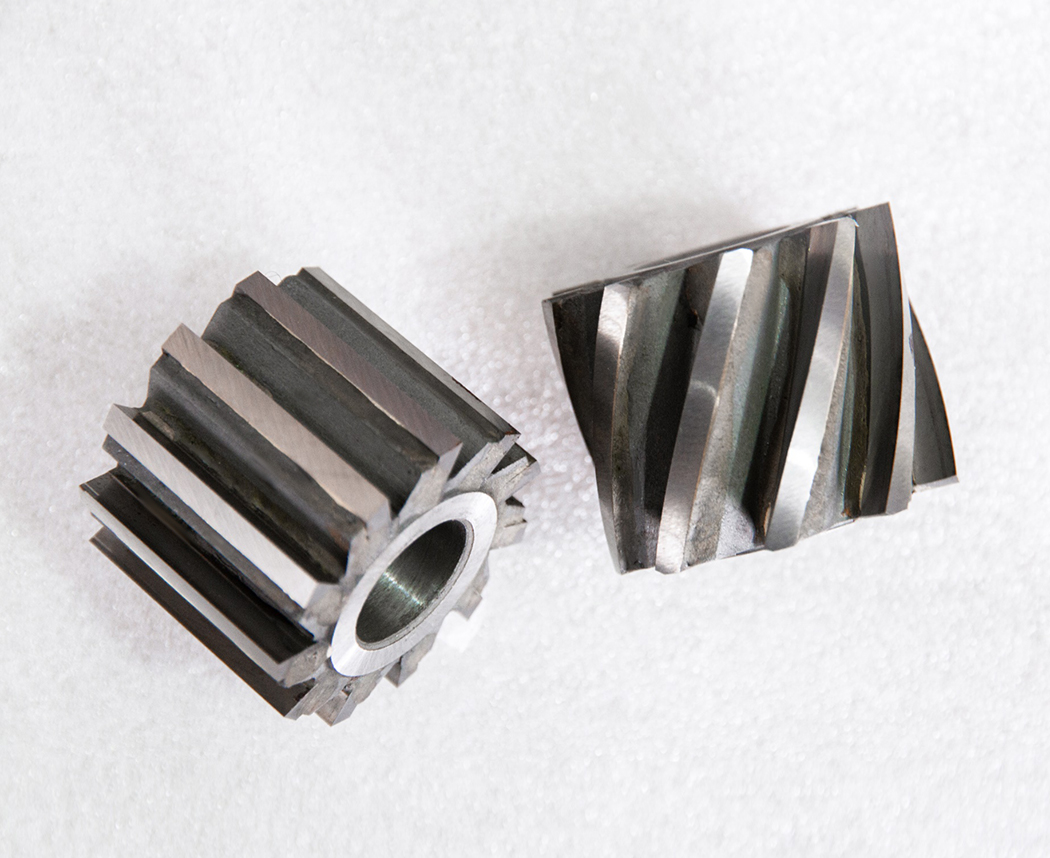
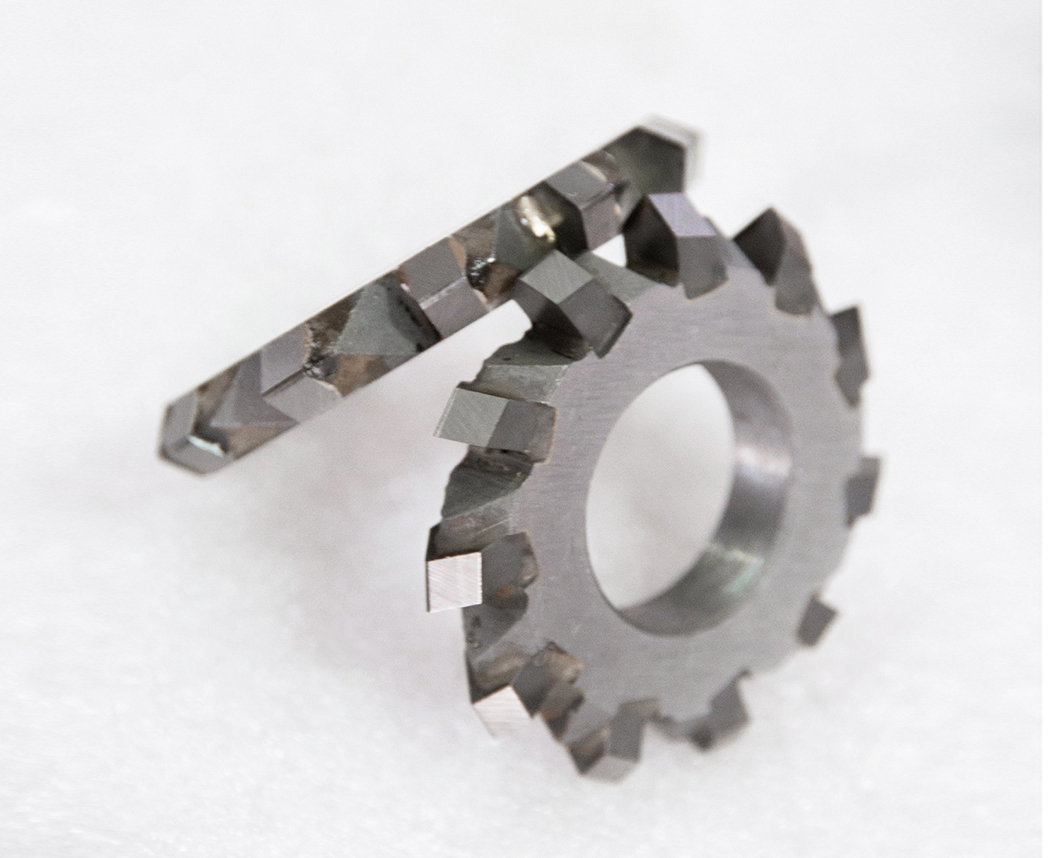
High speed steel saw blade milling cutters (conventional M2, M35, M42 cobalt containing high-speed steel) rely on good toughness and grindability, suitable for slotting, cutting, and slotting processing at medium and low cutting speeds and intermittent cutting. The suitable materials are as follows, and the selection differences and limitations are also marked:Sources:www.cssjlgj.com | PublishDate:2026.09.21
1、 Recommended processing materials
1. Ordinary carbon structural steel: Q235, 45 # steel, A3 steel. M2 high-speed steel is sufficient and widely used for cutting parts and narrow groove machining, with good cutting economy.
2. Low alloy structural steel: 40Cr, 20CrMnTi and other quenched and tempered/untempered low-alloy steels, suitable for conventional slotting and cutting; The quenching and tempering hardness should not be too high (generally ≤ 28HRC).
3. Stainless steel: 201, 304, 316 austenitic stainless steel, with priority given to M35/M42 cobalt containing high-speed steel. Cobalt enhances red hardness and reduces the risk of rapid wear and blade curling caused by cold work hardening during processing.
4. Copper and copper alloys: purple copper, brass, bronze. Large plasticity can easily lead to chip deposits, so it is generally recommended to use a large front angle tooth shape and cool it thoroughly.
5. Aluminum and aluminum alloys: pure aluminum, 6061, 6063, 5052, etc. The aluminum adhesive knife is obvious, using a large front angle, polished blade saw blade, and special cutting oil.
6. Cast iron: gray cast iron HT200, HT250. The material is brittle and the chips are in a fragmented state. It is recommended to choose a smaller front angle to prevent tooth breakage; Not suitable for high hardness ductile iron.
7. Engineering plastics, glued laminated boards: electric wood, fiberglass board PVC、 Nylon and other non-metallic materials have low cutting load, are not easy to burn, and M2 saw blades have strong versatility.
8. Soft non-ferrous metals: zinc alloy, magnesium alloy, suitable for low-speed slotting and cutting, with a focus on preventing knife sticking.
2、 Cautious processing (restricted scenarios)
1. Tempered and tempered high hardness steel: Tempered and tempered steel with a hardness greater than 30HRC has rapidly accelerated cutting wear and short tool life, and is generally not recommended. Hard alloy saw blade milling cutters are preferred.
2. Ductile iron: High hardness, strong abrasive properties, fast wear of high-speed steel saw blades, only suitable for small batch, shallow groove low-speed processing.
3. High temperature alloys and titanium alloys: high cutting temperatures and severe work hardening; Only suitable for small-scale testing and shallow cutting, not recommended for large-scale processing.
3、 Not suitable for processing materials
1. Hardened steel (HRC40 or above): High cutting temperature, insufficient red hardness of high-speed steel, and easy rapid wear, tooth breakage, and blade burning.
2. Hard alloy and ceramics: The hardness of the workpiece exceeds that of high-speed steel and cannot be cut.
3. High hardness wear-resistant castings: high chromium white cast iron, with extremely strong abrasive wear, and high-speed steel cutting tools quickly fail.