News Center
Recommending Products
Contact: Mr. Jin
Tel: 13901575780
0512-52428686
Contact: Mr. Zha
Tel: 13913639797
0512-52422071
Address: No. 59, Huyi Road, Liantang, Shanghu Town, Changshu City, Jiangsu Province.
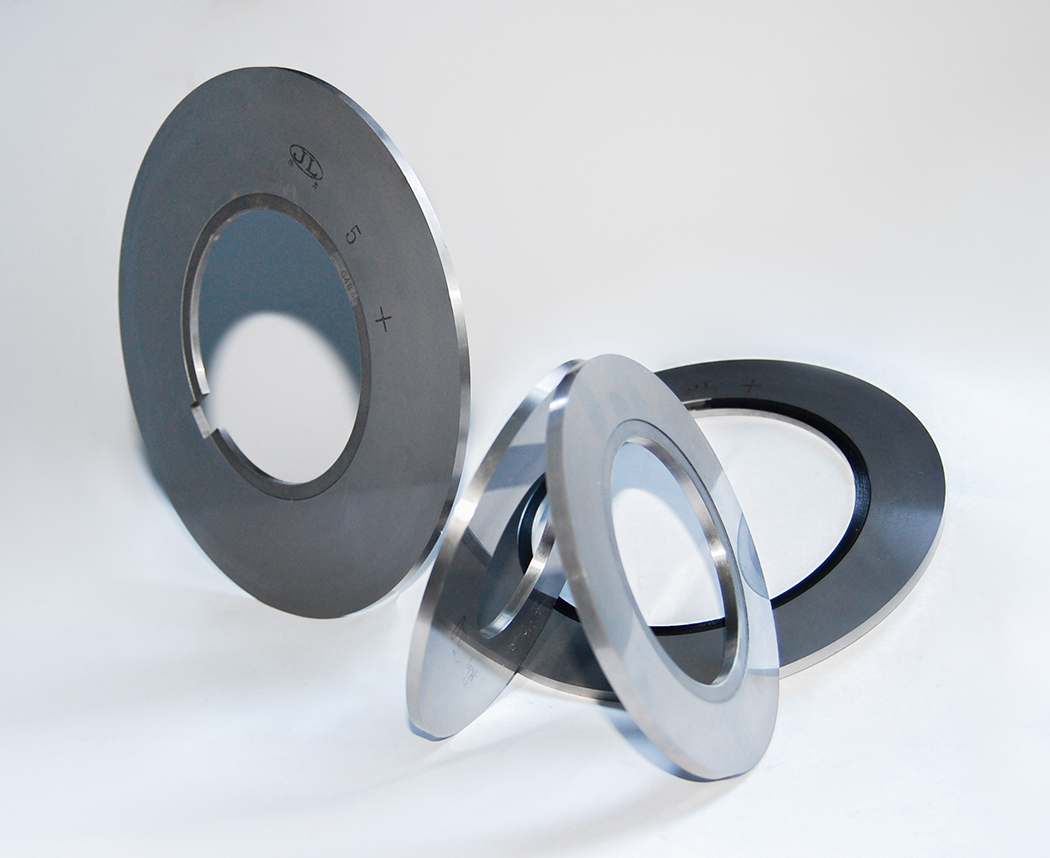
How to improve the service life of coated saw blade milling cutters
To extend the service life of coated saw blade milling cutters, multiple aspects such as substrate and coating selection, edge pretreatment, cutting parameters, clamping method, cooling and lubrication, workpiece working conditions, tool storage and grinding can be controlled.Sources:www.cssjlgj.com | PublishDate:2026.10.19
In terms of tool selection and pre preparation, match the corresponding substrate and coating system according to the processing material. High temperature resistant and anti-oxidation coatings can be used for processing materials that are prone to high temperatures, such as stainless steel and heat-resistant alloys; When processing plastic materials such as aluminum and copper, low friction coatings can be selected to reduce material adhesion. The coating thickness needs to be reasonably controlled, combined with edge passivation treatment, to eliminate micro notches on the edge and reduce the possibility of coating peeling under cutting impact. The number and shape of teeth need to be selected based on groove width, material characteristics, and machine rigidity to avoid cutting load concentration caused by unreasonable tooth density.
The reasonable setting of cutting parameters has a significant impact on the lifespan. The cutting line speed should be selected based on the heat resistance of the coating, and should not be continuously processed for a long time beyond the temperature tolerance range of the coating; The feed rate of each tooth remains stable. Excessive feed can easily cause tooth breakage, while insufficient feed can exacerbate blade friction and wear, resulting in chip deposits. The cutting process should be as smooth as possible to reduce hard impact and minimize damage to the cutting edge and coating caused by alternating thermal and mechanical stresses. When processing intermittent cutting conditions, the cutting speed can be appropriately reduced to buffer the fatigue loss caused by repeated cold and hot alternation.
Clamping and machine tool status control are equally important. Select tool holders and clamping washers with qualified accuracy, control the tool end face and radial runout. Excessive runout can easily cause single tooth overload, accelerate coating wear and tooth breakage. The tool overhang length should be shortened as much as possible while satisfying the machining depth, improving overall rigidity and suppressing cutting vibration. The locking torque shall be executed according to the specifications to avoid deformation of the saw blade caused by uneven pressure and uneven load wear. Before processing, check the clearance between the spindle and guide rail of the machine tool. The vibration of the machine tool will continue to impact the cutting edge, shortening the tool usage time.
Optimize cooling and lubrication schemes as needed. In scenarios where high temperatures are generated during continuous cutting, appropriate cutting fluids are used to remove heat, reduce the temperature in the cutting area, and slow down coating oxidation and wear; When selecting a micro lubrication method, it is necessary to confirm that the coating is suitable for the processing method. Cutting fluid needs to be kept clean to avoid mixing large amounts of hard chips and prevent them from grinding and scratching the coating on the cutting edge. When processing plastic materials, good lubrication can reduce the adhesion of the workpiece material to the tooth edge surface and minimize the continuous damage of chip deposits to the edge.
In terms of processing conditions and operation management, workpiece clamping needs to be stable to reduce workpiece vibration during the processing. Clean the oxide scale and hard spots on the surface of the workpiece before processing to avoid direct impact of the cutting edge on the hard surface. During the machining process, observe the cutting sound and surface quality of the workpiece. If there are abnormal noises or surface patterns, stop the machine for inspection in a timely manner to prevent minor damage from continuing to expand.
The storage, maintenance, and grinding of cutting tools also need to be standardized after use. Be well protected during storage to avoid scratches on the coating caused by blade collisions. Once the coating is damaged, the substrate is prone to rapid wear. Timely repair the tool after wear, control the grinding heat during the repair process, and avoid high-temperature damage to the substrate; After the grinding is completed, the coating treatment can be re applied to restore the cutting performance. Assess the degree of tooth damage before grinding, and tools with substrate cracks and extensive damage are not suitable for re coating and reuse.